asd

Showing posts with label structure. Show all posts
Showing posts with label structure. Show all posts
 Posted in:
إصلاح العيوب الإنشائية
إصلاح العيوب الإنشائية
يستعمل الحقن بالإيبوكسى لإصلاح شروخ الخرسانة المسلحة إصلاحا إنشائيا ،حيث يستعمل الإيبوكسى كمادة قوية تتمتع بمقاومة عالية للضغط وقوة تماسكها مع الخرسانة عالية .
ومن مميزاتة انه عندما يتم حقنه بطريقه سليمة فانة يعمر مدة طويلة لأنه يكون محميا داخل الكتلة الخرسانية من الإضاءة الشديدة أو دورات التجمد والذوبان أو الكيماويات أو البرى والمؤثرات الأخرى التى تقلل العمر التشغيلى للإيبوكسى فى معالجة الأسطح عند استخدامه فى سد الشروخ السطحية أو دهان الأسطح


طريقة التنفيذ:
1- تجهيز السطح : يتم فيها إزالة الخرسانة والمواد السائبة حول الشروخ وإزالة المواد التى ترسبت على السطح ويتم ذلك بتنظيف سطح الخرسانة بإستخدام الرماله .
2- حقن المياه :حقن المياه تحت ضغط يساعد على الأتى :
أ- تعقب التدفق ومسارته ب- قياس كميات التدفق ومعدلاته ج- تقدير مدى التدهور وانتشار الشروخ د- تنظيف الشقوق المتسعة من المواد السائبة
3- سد الشروخ السطحيه: يجب سد الأسطح الخارجية التى بها شروخ ولو كانت شروخا شعريه وتساعد عملية حقن المياه فى إظهار كل الأماكن المحتاجة الى سد سطحى ويجب ان تتحمل المادة المستخدمة فى سد الضغط المصاحب لعملية الحقن ولا يحدث تسرب للإيبوكسى الى الخارج ويستحسن أن تكون المواد المستخدمة فى السد السطحى ذات مرونة كافية ،بحيث لا يحدث بها شروخ تحت تاثير الضغط المصاحب للحقن
4-تركيب منافذ الحقن: يتم حفر الثقوب لتركيب منافذ الحقن فيها على الشروخ التى يسمح اتساعها لحقنها والتى يظهرمن فحصها أنها عميقه ومتصله بغيرها من الشروخ وتكون هذه الثقوب على مسافات من( 25-50 سم) حسب عرض الشرخ والعوامل الأخرى التى تؤثر على تدفق الإيبوكسي وكلما كان الشرخ أقل إتساعا كلما أصبح من الضرورى زيادة منافذ الحقل وتكون هذه الثقوب أعمق كلما زاد عمق الشروخ حتى يصل الإيبوكسى إلى التغلغل فى عمق الشرخ كله وفى حالة الشروخ غير العميقة يمكن إستخدام طريقة لحام حلمات على سطح الشرخ بدلا من عمل ثقوب بها وفى حالة الشروخ العميقة تركب حلمات الحقن عن طريق جلبة بحيث يتيح إتساع فوه الجلبة سرعة اكبر لتدفق الإيبوكسى فى الثقوب
5- ضخ الإيبوكسى: يبدأ ضخ الإيبوكسى من أسفل نقطة فى العضوويتقدم العمل لأعلى وفى بعض الحالات يفضل البدء فى أكثر الشروخ إتساعا ,وفى حالة الشروخ المملؤة بالماء فإن خروج المياه من المنافذ المفتوحة دليل على إحلال الإيبوكسى محل الماء ويتبع خروج الماء خروج سائل ابيض هو الراتنج المذاب فى الماء ويستمر خروج هذا السائل حتى يتحول لونه إلى لون الإيبوكسى فيتم غلق هذه المنافذ الواحدة تلو الأخرى بدون إيقاف عملية الضخ .
والضغط الازم لضخ الإيبوكسى يتناسب عكسيا مع إتساع الشرخ وعمقه ويتراوح الضغط بين (3إلى10كجم/سم2) والضغط المعتدل أو المتغير قد يكون أكثر كفاءة من الضغط العالى, والضغط الزائد عن الحد قد يتسبب فى إتساع الشروخ وزيادة التدهور أو تمزق الطبقة التى تسد الشروخ السطحية
2-إستبدال الخرسانة المعيبة أو زيادة القطاع الخرسانى:
الطرق المستخدمة
2-1-صب الخرسانة
2-2- رش الخرسانة
2-1-صب الخرسانة
عادة تستعمل هذه الطريقة فى حالة التدهور نتيجة الخرسانة المعيبة أو تسليح غير ملائم وإصلاح الأعضاء التى أصابها صدأ الحديد وإعادة تشكيل أوجه الكمرات والأعمدة
طريقة التنفيذ:
أ- إزالة الخرسانة المعيبة : يتم إزالة كل الخرسانة المعيبة مع تجنب الطرق العنيفة لقطع وإزالة الخرسانة ويستحن ان تكون المنطقة المزالة مقطوعة بالمنشار للحصول على جواف قائمة الزوايا وألا يقل عمق القطع عن اكبر مقاس للركام المستخدم فى الخرسانة الجديدة .
ب- رش الخرسانة القديمة بالماء : يجب ان يكون سطح الخرسانة القديمة نظيفا تماما حتى تتماسك الخرسانة الجديدة معه وان يكون مشبعا بالماء داخليا وجاف خارجيا والتشبع بالماء ضرورى لعمق كاف حتى لا تمتص الخرسانة القديمة الماء من الجديدة وللتاكد من تشبع الخرسانة القديمة بالماء لعمق كاف رشها برشاشات الماء لمدة 24ساعة قبل الصب .
ج- الدهان بالمواد اللاحمه : تستعمل مونة أسمنتية لا تجف بسرعة زمن شكها من(45-60دقيقة)ويتم خلط مونة الدهان فى خلاطات سريعة لتقليل الهواء الحبوس إلى أدنى ممكنة
وتسعمل راتنجات الإيبوكسى المتوافقة مع الماء كمادة لاحمة وهى الراتنجات التى يمكن دهانها على الاسطح الرطبة وتتميز بـ :
- يمكن تغير تركيبها بحيث لا تتصلد بسرعة وبالتالى تكون مناسبة فى الأجواء الحارة وفى حالة عمل الشدة الخشيبة
- تمنع تغلغل الكلوريدات من الخرسانة القديمة الى الجديدة بكفاءة عالية
د- إعداد الشدة : يجب أن تكون الشدة المستخدمة فى صب الخرسانة قوية وجاسئة لمنع الخرسانة الجديدة من التحدب بعيدا عن الخرسانة القديمة تحت تأثير وزنها وتحمل قوى الضخ فى حالة صب الخرسانة بالطلمبة وتحمل هزازات الشدة
وتعتبرالشدة الحديدية الثقيلة هى الشدة المثالية لأعمال الإصلاح
ه- تصميم الخلطة الخرسانية : جيب ان الخلطة الخرسانة المستعملة يسهل صبها ودمكها فى ظروف صعبة وأن تكون نفاذيتها قليلة وتحملها مع الزمن كبير
و- دمك الخرسانة الجديدة : للحصول على دمك جيد للخرسانة الجديدة يتم صب الخرسانة بكميات صغيرة ودمكها باستمرار مع تقدم العمل
رش الخرسانة
يتم رش الخرسانة بإستعمال مدفع الخرسانة وذلك بطريقتين :
1- الطريقة الجافة: حيث يتم خلط الأسمنت والركام على الناشف ثم يدفع بالخليط خلال الخرطوم حيث يقابل رشلش من الماء قبل خروجة من فوه التصريف
2- الطريقة الرطبة : حيث يتم خلط الركام والأسمنت والماء ثم يوضع الخليط فى طلمبة الخرسانة العادية التى تدفعه فى خرطوم حتى فوه التصريف مع اضافه مصدر للهواء المضغوط عند فوهه التثبيت لزياده سرعه الخليط حتى تحدث الالتصاق بالأسطح المرشوشه
* والطريقه الجافه هى الأكثر استخداما فى اصلاح المنشأت الخرسانيه حيث ان مقاومه طبقة الخرسانه تكون ضعف مقاومه طبقة الخرسانه باستعمال الطريقه الرطبه
زيادة مساحة صلب التسليح
وتعمل فى حالة قلة مساحة صلب التسليح عن 20% من المساحة الاصلية نتيجة الصدأ ويتتطلب الأمر فى هذه الحاله الى زيادة مساحة صلب التسليح بوضع اسياخ مستقيمة أو مكسحة أو إضافة الواح من الصلب لاستعاضة المساحة المفقودة
إضافة اسياخ أو كانات :
اسياخ التسليح المضافة إما ان تكون فى داخل القطاع الاصلى ، حيث يتم وضعها بعد إزالة الخرسانة المعيبة وتنظيف الحديد من الصدأ – أو توضع فى خارج القطاع الاصلى داخل القميص فى حالة الاعمدة والكمرات –أو طبقه جديدة من الخرسانة فى حالة البلاطات والحوائط
وتثبت اسياخ التسليح المضافة بالطرق الاتية :
أ-الركوب: وهى اسهل طرق نقل القوى من اسياخ التسليح الاصلية والمضافة ولا تقل مسافة الركوب عن 40 مرة قطر السيخ
ب-الوصلات: وتتم بوصل نهاية السيخ الاصلى ببداية السيخ الاضافى كجلبة أو ابزيم دوار
ج- اللحام : يراعى عدم لحام الصلب عالى المقاومة إلا فى نقاط محددة ، لان الحرارة العالية تفقده خواصه ويتحول الى صلب عالى
د- التثبيت: حيث تثبت الاسياخ المضافة فى الخرسانة بمسامير تثبيت من الصلب فى اماكن يحددها المهندس الاستشارى
ه-إضافة الواح الصلب: وتسخدم كبديل عن إضافة اسياخ أو كانات ويتم إضافتها بتثبيتها على السطح الخارجى للخرسانة وتثبت هذه الألواح بمسامير من الصلب تدفن فى فجوات فى الخرسانة ثم تملأ الفجوات بمادة لاحمة قوية أو يتم لحام هذه الألواح فى صلب التسليح الأصلى بعد إزالة الغطاء الخرسانى
طريقة لصق الألواح
1- يجب ان يكون سطح الخرسانة نظيفا وجافا وذا جوده عاليه
2- يتم تثبيت المسامير الصلب فى الفجوات المخصصه لها
3- يدهن سطح الخرسانه بطبقه رفيعة من راتنجات الإيبوكسى
4- تدهن الألواح الصلب أو تعالج بحيث تكون مقاومة للصدأ وتوضع الألواح فى الاماكن المحددة ،وتثبت فى مسامير الصلب بقلاوظ خاص بحيث تضغط على سطح الخرسانة
5- بعد تمام تصلد طبقة التماسك يتم إجراء إختبار سلامة أو نقص قوة الإلتصاق للتاكد من إلتصاق كل مساحة التماسك
William LeMessurier
William LeMessurier
installment loansBuilder of Elegant Cutting-edge Structures
Richard G. Weingardt, D.Sc. (h.c.), P.E., Dist.M.ASCE, F. ACEC
installment loans

Figure 1: William J. LeMessurier. Courtesy of Bill Thoen.
At his zenith, William ("Bill") James LeMessurier, Jr. (Figure 1) was known around the world as one of America’s most daring tall building designers. Based in Cambridge, Massachusetts, his firm’s list of outstanding projects included elite high-rises in all of the northeastern states and in many others scattered around the country. Internationally, several of his company’s more noteworthy projects were found in Egypt and in Middle Eastern countries like the United Arab Emirates, Saudi Arabia, Bahrain and Iraq. Although best known for skyscrapers, LeMessurier’s life-time body of work also included numerous civic and educational buildings, and a wide array of commercial and industrial facilities.
According to William Thoen, a long-time personal friend and professional partner, LeMessurier was a Renaissance man who collaborated with architects in such a way that "his structural organization and economy showed through in the finished work. In many cases, Bill worked closely with the architect from the concept stages to final design so that the project, while still the architect’s design, had the subtle structural harmony of form that the problem called for. He had an exceptional talent for interfacing with architects to make even their most difficult designs feasible."
Additionally, said Thoen, "Bill loved teaching as much as engineering, and was always at his best with an audience. He was extremely intelligent, insightful and highly articulate, and if you got into a verbal argument with him you would surely lose, usually in the first round. He thought very carefully about whatever he said and was precise in his use of language. I think that is what made him such a good leader, lecturer and teacher."
Bill was born on June 12, 1926 in Pontiac, Michigan, the youngest of four children of Bertha (Sherman) and William James LeMessurier, Sr., who owned a dry-cleaning business. After finishing high school, Bill left Michigan to major in mathematics at Harvard University, earning a Bachelor of Arts degree in 1947. He then studied architecture at Harvard’s Graduate School of Design, and received a master’s degree from Massachusetts Institute of Technology (MIT) in building engineering and construction in 1953.
While at MIT, LeMessurier worked part-time for Albert Goldberg, an established Boston structural engineer with a good reputation. Shortly after receiving his master’s, LeMessurier joined Goldberg full-time. By the mid-1950s, he had become a partner and the firm was renamed Goldberg-LeMessurier Associates.
In April 1961, the two separated, dividing up staff and clients, and Bill launched LeMessurier Associates. It began with a dozen engineers and draftsmen. In addition to 35-year-old LeMessurier, the new company’s partners were William Thoen, Emil Hervol and James Collins. Prominent among the firm’s early projects were elementary schools. From the very beginning, LeMessurier always gave his architectural clients innovative structural solutions whether projects were large-scale or minor in size.
For example, on a small school gymnasium project, the architect wanted to match the gable-roof shape and style of the other buildings on campus. Because the space was intended for basketball and other games, a deep ridgeline girder or tie rods at the knees of the frame were out of the question. Rigid frames were also ruled out because of cost and the architect’s objection to sub-floor tie rods. The LeMessurier solution? A funicular truss within both planes of the roof that spanned from end to end of the building, effectively taking advantage of the full depth of the slanted roof. Utilized in the system were laminated wood rafters, two continuous (draped and diagonally placed) flat steel bars secured to the rafters (one bar on each side of the roof) and a layer of plywood sheathing on top of the rafters (and steel bars) acting as a diaphragm.
For the Exeter, New Hampshire Athletic Center and Ice Skating Rink (Figure 2), the goal was to give visitors a clear view into the activity spaces from a galleria along a central spine, without having to look though a ceiling cluttered with structural framework. LeMessurier put the structural frame on the outside of the building, and hung the roof from it. This achieved maximum structural economy because deep structural
frames could be utilized.

Figure 2: Exeter, New Hampshire, Athletic Center. Courtesy of Bill Thoen.
One of LeMessurier’s first and longest-lasting architectural clients was Hugh Stubbins, a promising architect just appearing on the national scene in the mid-1950s. Said Thoen, "There were not a lot of structural engineers in the area then, and Stubbins came to Goldberg-LeMessurier one day for us to do an elementary school. As soon as Hugh and Bill met, there was a chemistry between them. Both were looking for excellence in their work. From then on LeMessurier became Hugh’s only structural engineer. Stubbins was sort of a destiny’s tot, and as his reputation grew, so did ours."

Figure 3: Singapore Treasury Building (aka Temasek Tower). Courtesy of Wikimedia Commons/Sengkang.
Representative of Stubbins-designed, high-profile skyscrapers engineered by LeMessurier were the 770-foot-tall Singapore Treasury Building (Figure 3) and the 920-foot-tall Citicorp Tower in New York City (Figures 4 and 5). The Treasury Building (aka Temasek Tower) has a round concrete spine or core that supports the entire weight of the building, from which the floors cantilever out 40 feet. One major element, its concrete tube, essentially provides all the required framing strength and rigidity needed for the entire building.

Figure 4: Citicorp Tower, New York City. Courtesy of Wikimedia Commons.

Figure 5: Base of Citicorp Center tower. Courtesy of Wikimedia Commons.
The unique base column configuration of the Citicorp Tower came about because of an unusual site constraint: St. Peter’s Church, which had sold its air rights but would not allow columns from any building above it to penetrate into its floor area. Instead, the new skyscraper’s four major corner columns were relocated to the center of the building’s four sides. From these side columns, the building edges were supported using large-scale chevron trusses.
The building required a light steel structure and lightweight glass and aluminum curtain walls, all of which had a very low mass. Although the building had sufficient strength, additional damping was needed to enhance structural performance and provide for better occupant comfort. A tuned-mass damper - the first use of such a damper in a major tall building - was the low-cost solution.
In June 1978, shortly after Citicorp Tower was completed and occupied, a potential weakness was uncovered. If hurricane-force winds - 70 miles an hour or more - hit it at a 45-degree angle, the building might be unsafe or unstable. First alerted to the problem by a Princeton University senior-class engineering student, Diane Hartley, LeMessurier revisited his structural design. In doing so, he discovered another aggravating issue: The building’s vital chevron trusses, originally designed to be welded, had been joined with weaker bolted joints, a cheaper method substituted during construction to save the owner money.
To eliminate the structure being vulnerable to a lethal problem from a severe hurricane and to provide for a higher factor of safety, LeMessurier oversaw a furious schedule of repairs in August 1978, in which drywall workers, carpenters and welders worked around the clock to strengthen and repair the flawed joints. Because of his quick actions in resolving the issue, stepping forward and taking responsibility whatever the consequences to himself or his reputation, most structural engineers today celebrate LeMessurier as an industry hero and a role model for ethics. David Fowler, the legendary University of Texas professor, reflects the general sentiment: "What LeMessurier did was absolutely the right thing."
In addition to Exeter, Singapore and Citicorp, representative of LeMesurier’s many other notable buildings are the National Air and Space Museum, Washington, DC; Dallas-Fort Worth Regional Airport, Texas; King Khalid Military City, Al Batin, Saudi Arabia; City Hall, Boston, Massachusetts; First Republic Bank Plaza, Dallas, Texas; Metro-Dade Administration Building, Miami, Florida; and Federal Reserve Bank, Boston, Massachusetts.
Robert McNamara, co-founder of McNamara-Salvia, who joined LeMessueier after receiving his master’s degree from the University of California at Berkeley, recalled LeMessurier’s skill in dealing with new engineers, especially with those like him having in-depth training in the use of the latest and greatest computer methods. "Bill took me under his wing and we applied this new technology to most of the new projects in the office. My experience working with Bill was certainly a highlight of my early career. He openly shared his experience and creativity, and I learned quickly the importance of looking at the total system from the start."
As time went on, LeMessurier developed a close association with the Harvard Graduate School of Design, and served in his later years as an adjunct professor who lectured Harvard graduate students on building design, emphasizing the need for a close relationship between architects and structural engineers.
An avid reader, LeMessurier also enjoyed playing the piano, which he did expertly. Although not a sailor, he owned a speedboat, which he used to get from the mainland to his retreat island on Lake Sebago in Maine - and which he often liked to operate at high speeds. Originally called "Doctor’s Island," LeMessurier’s private island was a quiet, remote, and out-of-the-mainstream place where he went to rest, relax and reflect.
Inducted into the National Academy of Engineering (NAE) in 1978, LeMessurier was made an honorary member of the American Institute of Architects (AIA) in 1988 and an honorary member of the American Society of Civil Engineers (ASCE) in 1989. He was also the recipient of an honorary degree in engineering from Rensselaer Polytechnic Institute. Among his many other prized awards were the 1999 Kimbrough Award from the American Institute of Steel Construction (AISC), 1996 President’s Medal from ASCE and 1968 Allied Professions Medal from AIA.
LeMessurier died on June 14, 2007, in Casco, Maine, at age 81. He was survived by his wife of 54 years, the former Dorothy Judd; by two daughters, Claire and Irene; by a son, Peter, a mechanical engineer; and by seven grandchildren.▪
William LeMessurier
structural designer of the Citicorp building, structural enginee
William J. LeMessurier, P.E.

William LeMessurier is a professional civil engineer, who is credited with combining daring design with innovative structure to create towering buildings that distinguish the skylines of America's great cities, including Boston, with the Federal Reserve Bank.
He was elected to the National Academy of Engineering, the highest honor of his profession, in 1978. His greatest distinction is that he took full responsibility for the near failure of the bracing system in New York's Citicorp Center tower. By putting his career and reputation on the line to correct the problem, Mr. LeMessurier prevented the catastrophic collapse of the building, saving lives and setting an example of positive ethical behavior.
His ethical leadership was reported in the article, "The Fifty-Nine-Story Crisis," published in the May 29, 1995 issue of The New Yorker magazine.
Mr. LeMessurier graduated from Harvard University, attended Harvard School of Design and received a master's degree from Massachusetts Institute of Technology in 1953. He also holds an honorary degree in engineering from Rensselaer Polytechnic Institute. Retired from LeMessurier Consultants Inc., he is an adjunct professor of architecture at Harvard GSD.
His other designs include Boston's State Street Bank, the Dallas-Fort Worth Airport, and the National Air and Space Museum in Washington D.C.
New Construction Materials for Modern Projects

S.A. Reddi, Deputy Managing Director (Retd), Gammon India Ltd.
India is witnessing construction of very interesting projects in all sectors of Infrastructure. High rise structures, under construction, include residential/commercial blocks up to a height of 320 m and RC chimneys for thermal power stations extending upwards up to 275m. Majority of the structures are in structural concrete. The functional demands of such high rise structures include the use of durable materials. High Strength Concrete, Self–compacting Concrete are gaining widespread acceptance. Apart from the basic structural materials, modern projects require a variety of secondary materials for a variety of purposes such as construction chemicals, waterproofing materials, durability aids etc. The paper highlights some of the recent developments.
Durable ConcreteConcrete Design and Construction Practices today are strength driven. Concrete grades up to M80 are now being used for highrise buildings in India. However, due to escalation in the repair and replacement costs, more attention is now being paid to durability issues. There are compelling reasons why the concrete construction practice during the next decades should be driven by durability in addition to strength.
A large number of flyovers and some elevated roads extending up to 20km in length are being realized in different parts of the country and involve huge outlay of public money. However, the concrete durability is suspect. Many of the structures built during the period from 1970 have suffered premature deterioration. Concrete bridge decks built during the period now require extensive repairs and renovations, costing more than the original cost of the project. Multi-storied buildings in urban areas require major repairs every 20 years, involving guniting, shotcreting etc.
A holistic view needs to be taken about concrete durability. In this context, there are a large number of materials in the market which facilitate durable construction. Apart from the materials, the construction processes have also undergone changes with a view to improving the durability of the finished structure.
High Performance Concrete
 In the United States, in response to widespread cracking of concrete bridge decks, the construction process moved towards the use of High Performance Concrete (HPC) mixes. Four types of HPC were developed1:
Very High Early Strength Concrete – 17.5 mPa in 6 hours
High Early Strength Concrete – 42.5 mPa in 24 hours
A Very High Strength – 86 mPa in 28 days
High Early Strength with Fiber Reinforcement
High Performance Concrete was introduced in India initially for the reconstruction of the pre-stressed concrete dome of the Kaiga Atomic Power Project, followed for parts of the Reactors at Tarapur and Rajasthan. Subsequently, a number of bridges and flyovers have introduced HPC up to M75 grade in different parts of India.
Self–compacting Concrete (SCC)SCC was developed by the Japanese initially as a Quality Assurance measure, but now is being widely used for concrete structures worldwide. In India, one of the earliest uses of SCC was for some components of structures at Kaiga Atomic Power Project. Many components of the structures were very heavily reinforced and the field engineers found it difficult to place and compact normal concrete without honeycombs and weaker concrete. SCC was successfully used.
SCC leaving the batching plant is in a semi-fluid state and is placed into the formwork without the use of vibrators. Due to its fluidity, SCC is able to find its way into the formwork and in between the reinforcement and gets self-compacted in the process. SCC is particularly useful for components of structures which are heavily reinforced. The fluidity is realized by modifying the normal mix components. In addition to cement, coarse and fine aggregates, water, special new generation polymer based admixtures are used to increase the fluidity of the concrete without increasing the water content.
Due to its high fluidity, the traditional method of measuring workability by slump does not work. The fluidity is such that any concrete fed to the slump cone falls flat on raising the slump cone; the diameter of the spread of concrete is measured as an indication of workability of SCC. This is called Slump Flow and is in the range of 600 – 800 mm.
Apart from the use of superior grade chemical admixtures, the physical composition of the concrete for SCC has undergone changes. The concrete is required to have more of fine aggregates and compulsorily any of the mineral admixtures – fly ash, ground granulated blast furnace slag (GGBFS), silica fume, metakaolin, rice husk ash etc. Fly ash is abundantly available as a waste product at all the thermal power stations and the Government has encouraged use of fly ash by offering them practically free at the thermal power stations. GGBFS is again a by-product of the steel mills. During the production of steel, a molten steel is poured from blast furnaces and travels in special channels, leaving the impurities on top of the stream. The waste material, being lighter moves on top and easily diverted away from the usable steel.
The diverted slag is quenched and forms small nodules. These nodules are crushed and granulated into very fine product, with particle size smaller than that of cement. The product is marketed in 50 kg bags and available economically in the regions around steel mills with blast furnaces. In other regions, additional transport cost of this bulk material is involved but its use is justified because of contribution to durability of concrete. For the concrete components of the structure for Bandra and Worli sewage outfalls in Mumbai, the German prime contractor insisted on compulsory use of GGBFS for the M40 concrete in order to improve the durability of concrete. GGBFS had to be transported from Vizag in the eastern part of India, in spite of heavy transportation cost. Since then GGBFS is finding widespread use in different parts of India for ensuring durable concrete.
The Use of Mineral Admixtures
 After realization of the need for durable concrete structures, the composition of concrete has undergone changes. From being a product made of three or four materials (cement, aggregates, water), today a typical durable concrete consists of six or more materials. The use of low water cement ratio enables a reduction in the volume and size of capillary voids in concrete; this alone is not sufficient to reduce the cement based content of concrete which is the source of micro-cracking from thermal shrinkage and drying shrinkage.
To reduce the cement based content, both the water content and cement content must be reduced as much as possible. Concrete mixes with fewer micro cracks can be produced by blending the cement with mineral admixtures either in the batching plant or in the cement plant. This enhances the service life of concrete structures in a cost-effective manner.
Fly AshThermal power stations are left with an undesirable by-product, fly ash, in large quantities which is not able to effectively utilize or dispose of. Currently, (2009) more than 120 million tonne of fly ash are generated annually and the storage and disposal has been costing the power stations substantial unproductive expenditure. Unfortunately, all the fly ash available at the power stations is not fit for use as mineral admixture directly. Fly ash as a mineral admixture should conform to IS: 3812. Such a material is available in the finer streams of Electro Static Precipitators fitted to the power generation system.
The coarser materials are required to be processed (generally with the help of Cyclones) before being considered for use as mineral admixture for concrete. There are only a few processing units in India, including the one as Nashik Thermal Power Station. As per the Euro Code for Concrete, only processed fly ash can be permitted as mineral admixture in concrete. The code limits the use of fly ash. About 35% of cement may be replaced by fly ash; the actual percentage replacement depending on the outcome of trial mixes.
High Volume Fly Ash Concrete (HVFA)The high volume fly ash concrete (HVFA) represents an emerging technology for highly durable and resource efficient concrete structures. Laboratory and field experience have shown that fly ash from modern coal-fired thermal power plants, when used in large volume (typically 50 - 60% by mass of the total cementitious materials content, is able to impart excellent workability in fresh concrete at a water content that is 15 – 20% less than without fly ash. To obtain adequate strength at early age, further reductions in the mixing water content can be achieved with better aggregate grading and use of super-plasticizers.
HVFA concrete has now been successfully used in a few sporadic projects in India. All SCC in India use HVFA, to the extent of 50% cement replacement. Some concrete roads being built by NHAI have also used HVFA concrete, including the Four-Laning of Satara – Kolhapur National Highway.
Ground Granulated Blast Furnace Slag (GGBFS)The problems associated with the quality of fly ash do not exist in the case of Ground Granulated Blast Furnace Slag GGBFS, as the produce is necessarily the outcome of grinding to the required particle size. Thus the use of GGBFS as a mineral admixture should be preferred, despite long leads for end users in certain parts of India far from the steel plants. GGBFS sold in India is of uniform quality and particle size gradation. For many landmark structures such as the Burj Dubai (the tallest building in the world in 2009) GGBFS has been extensively used as a mineral admixture, even though the material is imported from other countries, resulting in the landed cost being more than that of cement. This was a conscious decision with a view to obtaining a more durable concrete structure.
In India the use of GGBFS has been fairly limited, in spite of all the technical advantages. The Indian Concrete Code permits up to 70% of cement replacement where GGBFS is used. Technically, the use of GGBFS is more effective only at replacement levels of 50% or more. For a number of structures in a port in Andhra Pradesh, typically the M40 concrete mix contained 100 kg of cement and 300 kg of GGBFS.
Portland Slag Cement (PSC) is also available and useful for ensuring durability of concrete structures. Due to the proximity to steel mills, PSC is generally produced in locations close to steel plants. Here again due to the bulky nature of the product, the transportation cost predominate. Another issue concerning quality of the PSC is the actual percentage replacement while making PSC; this information is not normally displayed on the bags, leaving the user at a disadvantage. In developed countries, information regarding the percentage of slag utilized in making PSC is generally printed on each bag of cement.
Condensed Silica Fume (CSF)
 CSF is a by-product of Ferro-Silicon industry and at present an imported product, easily available in the Indian market. The particle size is very small, about 100 times smaller than that of cement. It can occupy the voids in between cement particles in a concrete mix, reduce the water demand and thus contribute to a very dense concrete of high durability. Normally, 5 - 10% of cement can be replaced by CSF in order to produce durable concrete. The product is expensive and is used in developed countries only for very high strength concrete (above 75 mPa). Indiscriminate use of CSF for lower grades, barring exceptions, only increases the project cost without corresponding technical benefits. Even when used, the percentage replacement should be based on trial mixes in each case, which may vary from one to 10%. CSF may also be used for High Performance Concrete of lower grades.
Ternary BlendsTernary blends of mineral admixtures are now recommended for improving the durability of important concrete structures. An outstanding example is the Reconstruction of the New I-35 W St. Anthony Falls Bridge crossing the Mississippi River in Minneapolis, US. The new bridge has been opened to traffic in September 2008, less than 14 months after the collapse. HPC has been used for reconstruction with a target 100 year life span. High Performance Concrete containing silica fume and fly ash was used for low permeability.
Two gleaming white concrete sculptures tower 9 m high at each end of the bridge. The sculptures were pre-cast using an SCC mix that included photo-catalytic cement with self cleaning and pollution reducing characteristics. The photo-catalytic cement is one of the new developments in the construction materials industry. The SCC concrete resulted in a marble-like, smooth white finish to the concrete surface. With a low water cementitious material ratio (w/cm), air entrainment and a rapid chloride permeability test (RCPT) value of less than 1500 coulombs at 28 days, the monument will also be a durable feature in the severe environment adjacent to the I-35 W Roadway.2
For the drilled shaft foundations of the I-35 Bridge, SCC was used. To control temperature during curing, fly ash and slag were incorporated as the majority of the cementitious material. This reduced the heat of hydration by approximately 50%. The concrete mixes for the footings and piers were proportioned for mass concrete and durability through the use of fly ash and slag. As the components were massive in size, concrete mixes were modified by cementitious materials, chilled water and cooled aggregates, use of form insulation and internal cooling pipes.
Cement SilosThe use of batching plants for producing concrete is gaining increasing acceptance. As large volumes of cement are used in a batching plant, the cement is generally stored in vertical steel silos. When cement is received in bulkers from the factory, the same is directly pneumatically pumped into the silos which have capacities ranging from 50 to 500 tonne depending upon the project requirements. If only bagged cement is available, they are emptied into the silos, usually with the help of screw conveyors. For modern applications, more than one silo will be required depending on the types of cement and mineral admixture used in the concrete mix.
In a recently commissioned batching plant complex in the Middle East, each of the two plants feature nine cement silos for Portland cement, slag cement, micro silica, fly ash and SRC cement.
Durability Enhancing ProductsA full line of products are available to prevent or repair corrosion damage. A typical corrosion inhibiting admixture prevents deleterious expansion and cracking caused by the formation of rust during over-induced corrosion. There are also penetrating sealants to protect new and repaired concrete from the corrosive effects of chloride. The silane and siloxane based reacting sealers soak into the surface, creating a barrier against water or chlorides.
A number of concrete waterproofing admixtures eliminate the need for conventional external waterproofing membranes and saves time, money and hassle at the construction site. It transforms concrete into a water-resistant barrier by becoming an integral part of the concrete matrix.
Hydrophobic Concrete Waterproofing SystemA typical patented product uses three materials to achieve a water-tight concrete structure, a super-plasticizer which reduces batching water requirements, thus limiting the volume of the capillary pour network in the concrete; a reactive hydrophobic pour blocking concrete admixture and product specific water stop protection at construction dams.
Other accessory products include an operation retardant, curing compound, water stops and polypropylene fiber reinforcement. The patented product is typically added while concrete mix is being prepared to assist waterproofing. One product is applied at the rate of 5 liter per of concrete. Typically the manufacturer provides a warranty period of 10 years. The performance warranty provides for repairing water leakage through industry accepted and approved means for a period of 10 years. The product however has some negative impact on the rate of gain of strength of concrete. As a rough indication, the specified characteristic 28-day strength of concrete will not be achieved at 28 days but at 56 days or more.
The cementitious content of concrete using the integral waterproofing compound shall not be less than 325 k g / c u m with up to 50% fly ash or slag replacement. The water cement ratio shall be adjusted to compensate for the water in the waterproofing compound and super-plasticizer and maintain the required workability. The water cement ratio shall not exceed 0.42. The product is of American origin, represented by an Indian company which provides the necessary technical expertise.
Reinforcement
 The revised BIS Code 1786 provides for four grades of reinforcement characterized by the yield strength – Fe 415, Fe 500, Fe 550 and Fe 600. Each of the first three grades is also available with superior ductile properties and a nomenclature is Fe 415D, Fe500D and Fe550D. Primarily the ductile grades specify a higher elongation value. Use of higher grades reduces the tonnage of steel in compression members e.g. columns substantially, results in decongested reinforcement and facilitates easy placement and vibration of concrete. Fe 415 and Fe 500 are easily available in the market. Fe 550 is now being offered by some prime producers–Tata Steel, Sail etc. After the revision of the Code, Fe 550 is also offered in selected diameters.
Fe 500 bars are now used for a number of highrise buildings, bridges and flyovers in India. Lapping of bars results in congestion of steel creates difficulties in proper placement and compaction of concrete and of course more expensive for large diameter bars. Couplers are now preferred instead of lapping. With widespread use, the cost of couplers has come down. The coupler design and manufacture permits the joints in the same plane without the need for staggering as in the case of lapping Fig. 1 shows typical use of couplers for columns of a multi-storied building in Mumbai.
Ternary Blended Cements
 Ternary blended cements containing the combination of fly ash–slag, fly ash–silica fume or slag–silica fume are commonly used for concrete in many parts of the world. The European Standard EN 197 for cement lists 27 different combinations for cement. Usually mineral admixture used may present a complimentary effect on cement hydration. Limestone filler addition produces favorable effects on cement test. In particular, the physical effects caused by limestone filler enhance the strength due to hydration acceleration of Portland clinker gains at very early age and the improvement of particle packing of the cementitious system. However, the rate of hydration is initially lower than that corresponding to Portland cement; shows a reduction of strength at early age and similar or greater strength at later ages. Ternary cements containing a limited proportion of limestone filler (no more than 12%) and 20 – 30% GGBFS provide a good resistance to chloride ingress and good performance in sulphate environment of low C3A Portland cement.4
Photo-catalytic CementThis is a patented Portland cement developed by Italcementi Group. The photo-catalytic components use the energy from ultra-violet rays to oxidize most organic and some inorganic compounds. Air pollutants that would normally result in discoloration of exposed surfaces are removed from the atmosphere by the components, and the residues are washed off by rain. This cement can be used to produce concrete and plaster products that save on maintenance cost while they ensure a cleaner environment.3
In addition to Portland cement binders, the product contains photo-catalytic titanium dioxide particles. The cement is already being used for sound barriers, concrete paver blocks and façade elements. Other applications include pre-cast and architectural planners, pavements, concrete masonry units, cement tiles etc.
Insulated Concrete Form (ICF)ICF structural elements allow maximum clear spans. The ICF elements are used for large commercial buildings, residential buildings etc.
Exterior Self–leveling Concrete ToppingThis is a Portland cement based product for fast track resurfacing and smoothing of concrete. It produces a smooth flat hard surface and dries quickly without shrinking, cracking or spalling. Pourable or pumpable when mixed with water, it installs 6 to 20 mm thick in one application and up to 50 mm thick with the addition of aggregate. It is pourable or pumpable when mixed with water. It can be used on, above or below grade and it makes spalled or damaged concrete look like new. Once sealed it creates an excellent wearing surface.
Carbon Dioxide (CO2)As part of a future global atmospheric stabilization strategy, industrialized countries may lead to use large amounts of carbon dioxide. CO2 may be used for curing pre-cast concrete units. Manufacturers of concrete masonry units could use CO2 to reduce energy consumption. Steam curing which is conventionally used is energy intensive. Although CO2 curing provides slower strength development than steam curing, the performance can be improved if the blocks are properly pre-conditioned before CO2 curing. It has also been noted that the water absorption of CO2 cured blocks is lower than that of steam cured blocks.
Corrosion Inhibiters for Reinforced Concrete
 Calcium nitrate has been proven to inhibit reinforcement corrosion. About 3–4% calcium nitrate of cement by weight is sufficient to protect the reinforcement steel against corrosion. Typically a corrosion inhibiter should
raise the level of chlorides necessary to initiate corrosion or
decrease the rate of corrosion after it has started or
both. Since it does not necessarily prevent corrosion from happening altogether, it is more appropriate to call the product as corrosion retarders.
Coarse Aggregates for ConcreteThe BIS Code (IS:383) permits the use of three types of coarse aggregates–natural gravel (shingle), crushed stone or a blend of both. Many outstanding structures built in India in the past had used river gravel as coarse aggregate for concrete including dams (Bhakra), prestressed concrete aqueducts and siphons (Kunu Siphon), large number of prestressed concrete bridges, power stations (Trombay 500 MW Unit V) etc. The results are excellent. Use of rounded aggregates, by virtue of their geometry, reduces the cement and water content requirements of concrete, thus contributing to the economy. Almost 50% of all the concrete produced in the developed world utilizes natural gravel and broken stone is used only when gravel is not available within economic leads.
Recycled AggregatesWith continuous development activity worldwide, the availability of coarse aggregates from natural sources or crushed rock are dwindling; at the same time, due to demolition of old structures, roads etc., a large amount of debris is generated annually and their disposal poses problems for the individuals and the Governments. In many countries including the UK, any demolition agency is not permitted to dispose of the debris except at predetermined locations which may involve very long leads, expensive operations.
Extensive research has now established that the debris can be crushed, processed and recycled as coarse aggregate for fresh concrete. Such recycling solves the above mentioned problems of disposal, and also more economical. Many national codes in the developed world permit the use of recycled aggregates in concrete, subject to safeguards.
Lightweight AggregatesThese are manufactured products and are extensively used in all types of structures involving longer spans where the dead-load forms a major component of the loads involved in the design. Such lightweight aggregates are manufactured products using expanded clay, sintered fly ash etc. Their contribution to strength depends on the type and quality of the lightweight aggregate, the size fraction used and the amount of aggregate used as well as the type and quality of binder in concrete. However, the addition of lightweight aggregate in concrete reduces the modulus of elasticity.
High Performance Lightweight Concrete
 By using high strength/high performance lightweight concrete in prestressed concrete bridge girders, spans of bridge girders can be extended by up to 20%. The implications of using lightweight aggregate on prestressing losses long-term creep and shrinkage deformation should be considered. Compressive strength of up to 75 mPa has been obtained. They also result in reduction in creep and shrinkage and consequently lower prestressed losses. The overall costs for a given load capacity are reduced. The reduction in the structure dead-load leads to a reduction in the foundation size.
Self–curing, Shrinkage-free concreteItalian researchers have produced a concrete by the combined use of
a water reducing admixture based on polycarboxylate in order to reduce both the mixing water and cement.
a shrinkage reducing admixture
an expansive agent based on a special calcium oxide.The combined use of an expansive agent and a PC based water reducing super-plasticizer results in a shrinkage-free concrete even in the absence of any wet curing. Due to the water reduction caused by the PC based super-plasticizer at a given w/c, there is a reduction in the volume of cement paste and a corresponding increase in the amount of aggregates. Both are responsible for significant reduction in the drying shrinkage.
Advanced Composite ReinforcementIn highly corrosive environments, the use of advanced composite fiber reinforced polymers (FRP) is attractive as a replacement for conventional steel reinforcements. While the FRP materials can be resistant to corrosion, there is lack of ductility. At the moment FRP reinforcement in India is quite expensive. The main market for FRP in India is for structural retrofit for increasing the load capacity, to remedy construction defects or repair damages.
Application of Nano TechnologyReducing particle size of a material to nano–scale often imparts new properties or enhances existing ones. This is typical of nano particles of titanium dioxide, which maintains its photocatalytic activity even when mixed with cement. External cement based surfaces become strongly photocatalytic, leading to a much better appearance and a significant reduction in concentration of pollutants in the surrounding air.
The photoactive titanium dioxide was found to be a more powerful photocatalytic agent when its particle size decreased to non size. This makes it a ideal vehicle for application in construction. A cement binder containing about 5% of active titanium dioxide produces concrete with a smooth surface and also converts the pollutants, removes them from the surrounding air. In a typical application on a building in France completed in 2000, the quality of concrete surface have remained unchanged till date. The structure looked as if it were freshly built (Fig 3.)
Cleaner Surfaces and Less PollutionMixing active titanium dioxide with cement produces a binder that maintains its entire normal performance characteristic when used to make concrete. The photocatalytic action makes the surfaces not only to a significant self–cleaning; it also improves the quality of surrounding environment. Using titanium dioxide in glass fiber reinforced concrete offers more efficient and economical way to achieve the benefits of photocatalytics. The environmentally active e-GRC offers the most economical way to achieve cleaner, brighter facades.
Applications for the e-GRC include
Cladding panels and facades elements
Permanent formwork and form liners
Roofing tiles
Motorway and Railway sound barriers
References
Goodspeed, Vanikar & Cook “High Performance Concrete defined for Highway Structures,” Concrete International Vol. 18 No.2, Feb. 1996.
Alan R. Phipps, FIGG Bridge Engineers Inc “HPC for 100 Year Life Span,” HPC Bridge Views, FHWA Issue 52, Nov/Dec 2008.
Concrete that cleans itself and the air,” Concrete International Feb. 2009 Vol. 31 No. 2, The Magazine of the American Concrete Institute.
Irassar et al “Durability of Ternary Blended Cements containing Limestone Filler and GBFS,” ACI Publication SP-234, 2006.
Peter J M Bartos, e-GRC, CONCRETE, UK April 2009

Mixed-use Bridge for Amsterdam / Laurent Saint-Val
Mixed-use Bridge for Amsterdam / Laurent Saint-Val
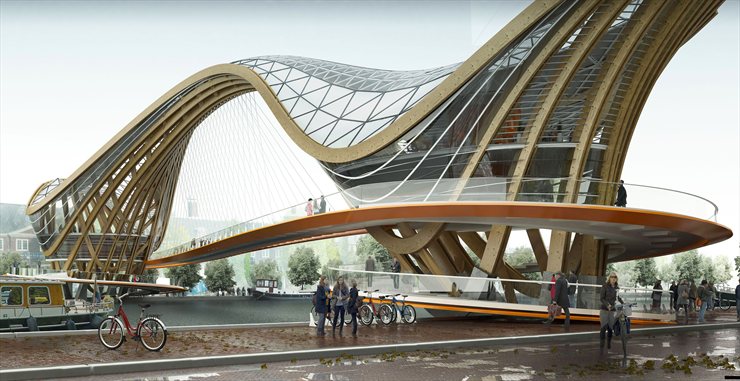
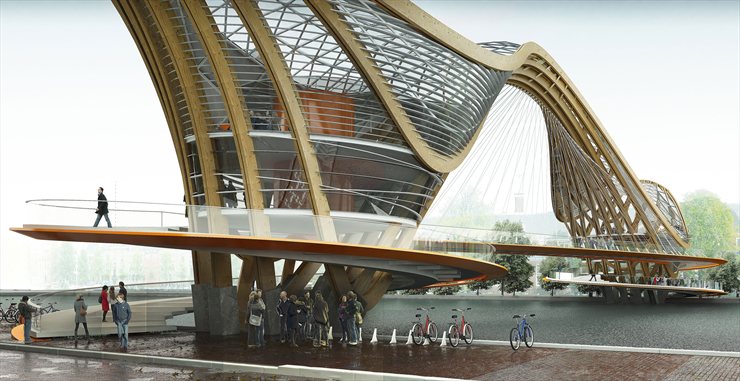
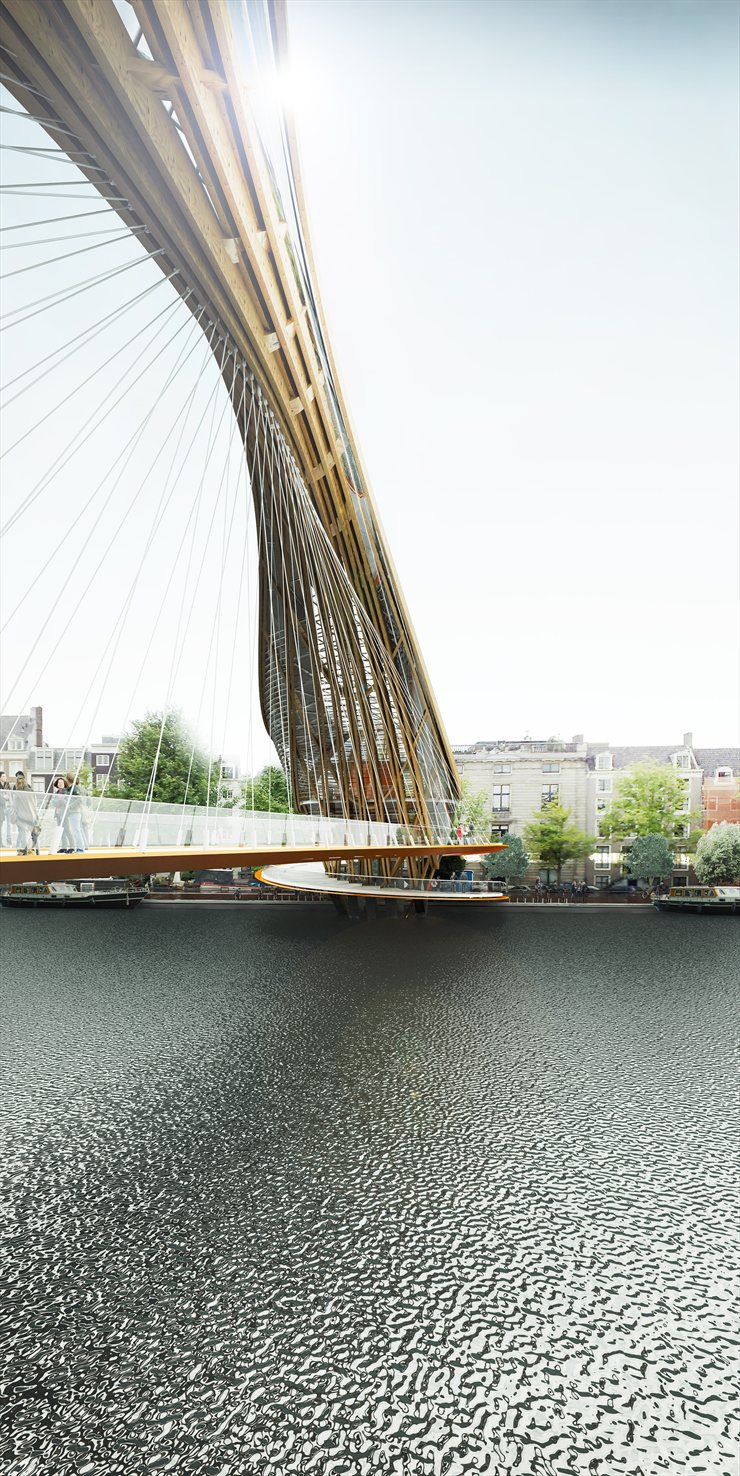
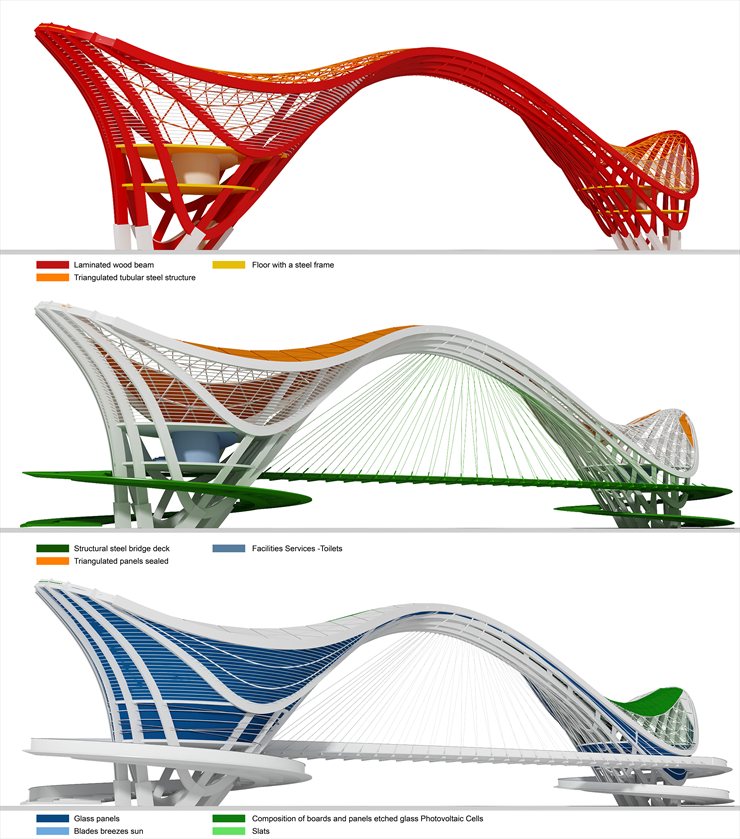
Architect Laurent Saint-Val proposes a new inhabitable bridge for Amsterdam. Fascinating mix of architecture with its 17th century’s canals registered at UNESCO World Heritage, AMSTERDAM, capital of Netherlands is the largest city of the country with a population of nearly 740 000 inhabitants (1.5 million with the periphery) and the most visited one with more than 3.5 million foreign visitors each year. It’s in the 12th century that the Dutch first settled in this marshy and inhospitable region that would become Amsterdam. 500 years later, during the 17th century, Amsterdam became the center of the world’s economy. Today, the Batavian capital is known worldwide for its openness to the rest of the planet, its tolerance and its bustling cultural life. Adventurer’s city, fishermen’s town, city of excess and extremes ; from a huge mansion to the narrowest house, modern architecture is developing between the historic building’s facades, giving a particular outcome and amazement for tourists. Due to the small size of the city, all interesting sites are within in a small area, making the visit even more agreeable. This is probably one of the reason why Amsterdam is so popular amongst poetry and architecture lovers. Wherever you walk in Amsterdam, you will notice that all constructions are made of brick. Never the less, it has not always been so, the houses were originally made of wood. Following the devastating fires of 1421 and 1452, it was forbidden to build with wood. In 1669, wooden construction was completely banned and only two examples are left standing. Undoubtedly, a knowledge and an architecural wealth slumber in the heart of the true Amsterdammers, ready to wake and be materialized in modern projects. It is with a strong motivation and a desire to pay homage to wood that I made the choice to use this modern material, ecological but also traditional and universal throughout centuries ; a material occupying a leading position with its qualities of sustainability, flexibility, adaptation to other materials, efficiency and finaly its esthetics. Wood, a traditional and universal material throughout centuries, has found the past few years a leading place, thanks to ecology. Therefore, every project today and particularly in Amsterdam cannot ignore the use of wood for new structures or ornament. Interior and exterior designs of this bridge are intended descriptive, while highlighting the natural material. Associated with steel and aluminium it gains enormous advantages, since these metals generate extremely light structures, representing a vital aspect regarding the soil’s quality.
Remarkable building material, steel can withstand heavy loads and can cover larger litters with smaller sections. For a simple mounting of bolts, rivets or welding corresponds a consequent simple removal system that facilitates additions, transformations, amputations, adaptations or even partial moves of a structure. As for glass, it allows me to play with shapes with elegance and give way to my creativity. In addition, we have access to multiple choices of glass : toughened, laminated, anti-burglary, insulation and many more… Large windows let in light and allow to have beautiful views of the outside ; not feeling trapped, able to blend with old or new constructions. Enjoy light and make the best use of it while meeting safety requirements. The easy access for all of this gateway open on each bank should revitalize this neighborhood and create an attractive link for this museum, slowly linking visitors towards this place of “culture” while also being a place of exchanges between populations, of casual conversations, of relaxation, of escapes and walks for every age.
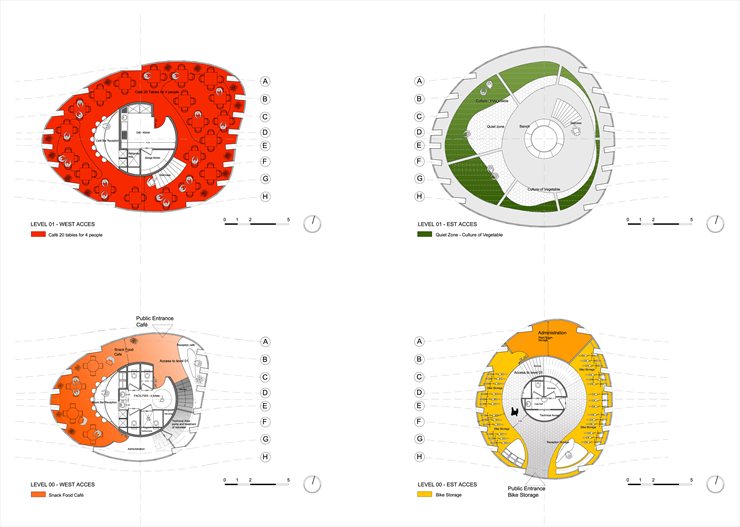
Closer to the museum, on the first floor is the bike shop and on top a garden. The garden accompanies man in all civilizations and does not start its history in a house. Space giving free rein to imagination, space for reflection and meditation, a sort of passive confrontation between mortals and continuous rebirth of nature. The philosopher Foucault saw in the garden a “space of located utopia”. Today, especially in this town, we talk more and more about bicycle as a gentle mean of transportation and an alternative to automobile for commuting. Bicycle escapes the ravages of time and despite the development of locomotion techniques, it retains its appeal if not its magic. This characteristic primarily applies itself in urban areas. In traffic that invades large cities, the major problem is pollution. Bikes don’t pollute and create a subtle relationship between man and his environment. Hence the value of this bike shop open to anyone who wants to introduce to his house the necessary practice to maintain a physiological balance for a city life more and more hectic. On the other bank a cozy cafe and its restaurant at the top level should in my opinion attract customers wishing of meetings and make these moments exceptional. To me, it seemed that a strong idea is a form of enchantment through the building and to what it can bring inside or from the outside. This gateway strong of its own identity, its European and contemporary character would be a welcoming site for all, a place of openness for today and tomorrow’s world with men and women that travel more and more, that became experts and can compare, that want excellence and should be seduce all the time.
Closer to the museum, on the first floor is the bike shop and on top a garden. The garden accompanies man in all civilizations and does not start its history in a house. Space giving free rein to imagination, space for reflection and meditation, a sort of passive confrontation between mortals and continuous rebirth of nature. The philosopher Foucault saw in the garden a “space of located utopia”. Today, especially in this town, we talk more and more about bicycle as a gentle mean of transportation and an alternative to automobile for commuting. Bicycle escapes the ravages of time and despite the development of locomotion techniques, it retains its appeal if not its magic. This characteristic primarily applies itself in urban areas. In traffic that invades large cities, the major problem is pollution. Bikes don’t pollute and create a subtle relationship between man and his environment. Hence the value of this bike shop open to anyone who wants to introduce to his house the necessary practice to maintain a physiological balance for a city life more and more hectic. On the other bank a cozy cafe and its restaurant at the top level should in my opinion attract customers wishing of meetings and make these moments exceptional. To me, it seemed that a strong idea is a form of enchantment through the building and to what it can bring inside or from the outside. This gateway strong of its own identity, its European and contemporary character would be a welcoming site for all, a place of openness for today and tomorrow’s world with men and women that travel more and more, that became experts and can compare, that want excellence and should be seduce all the time.